Prepared by: Arkmex · Content updated:
General planning guidance; a machine-specific survey and the agreed technical scope take precedence. Official references are listed below.
Engineering takeaways
- Change one verified condition at a time and keep a record of the result; random parameter changes hide the real cause.
- Change one verified process variable at a time and keep a labeled sample.
- A visible defect is evidence to investigate, not proof that more laser power is needed.
Record a repeatable fault sample
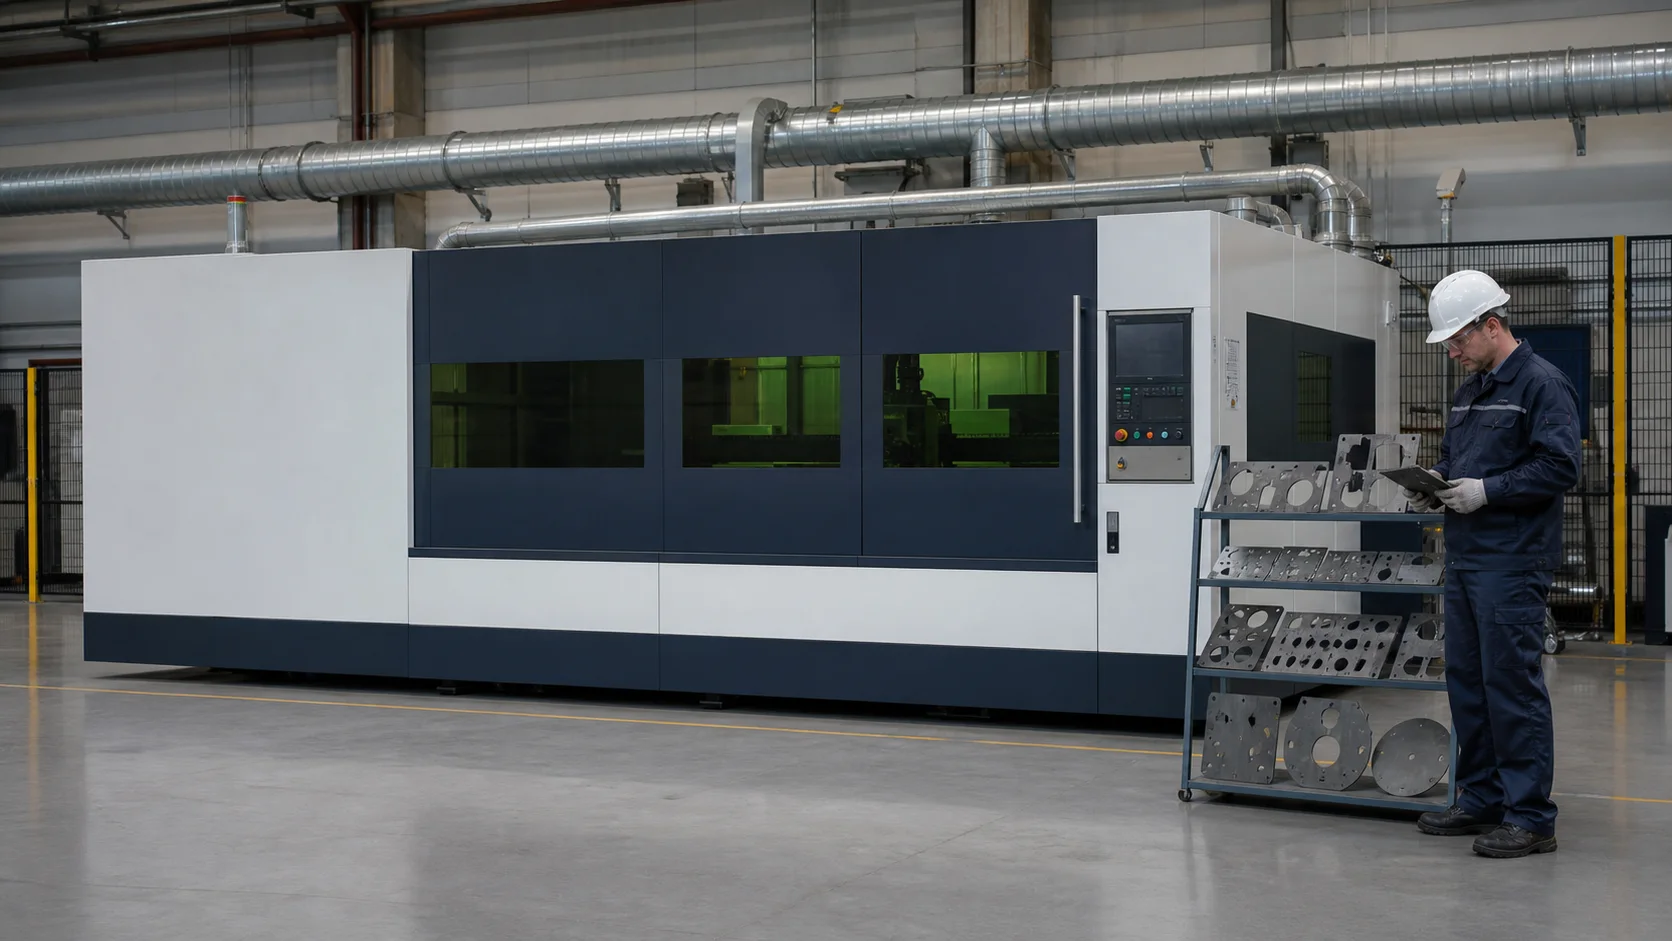
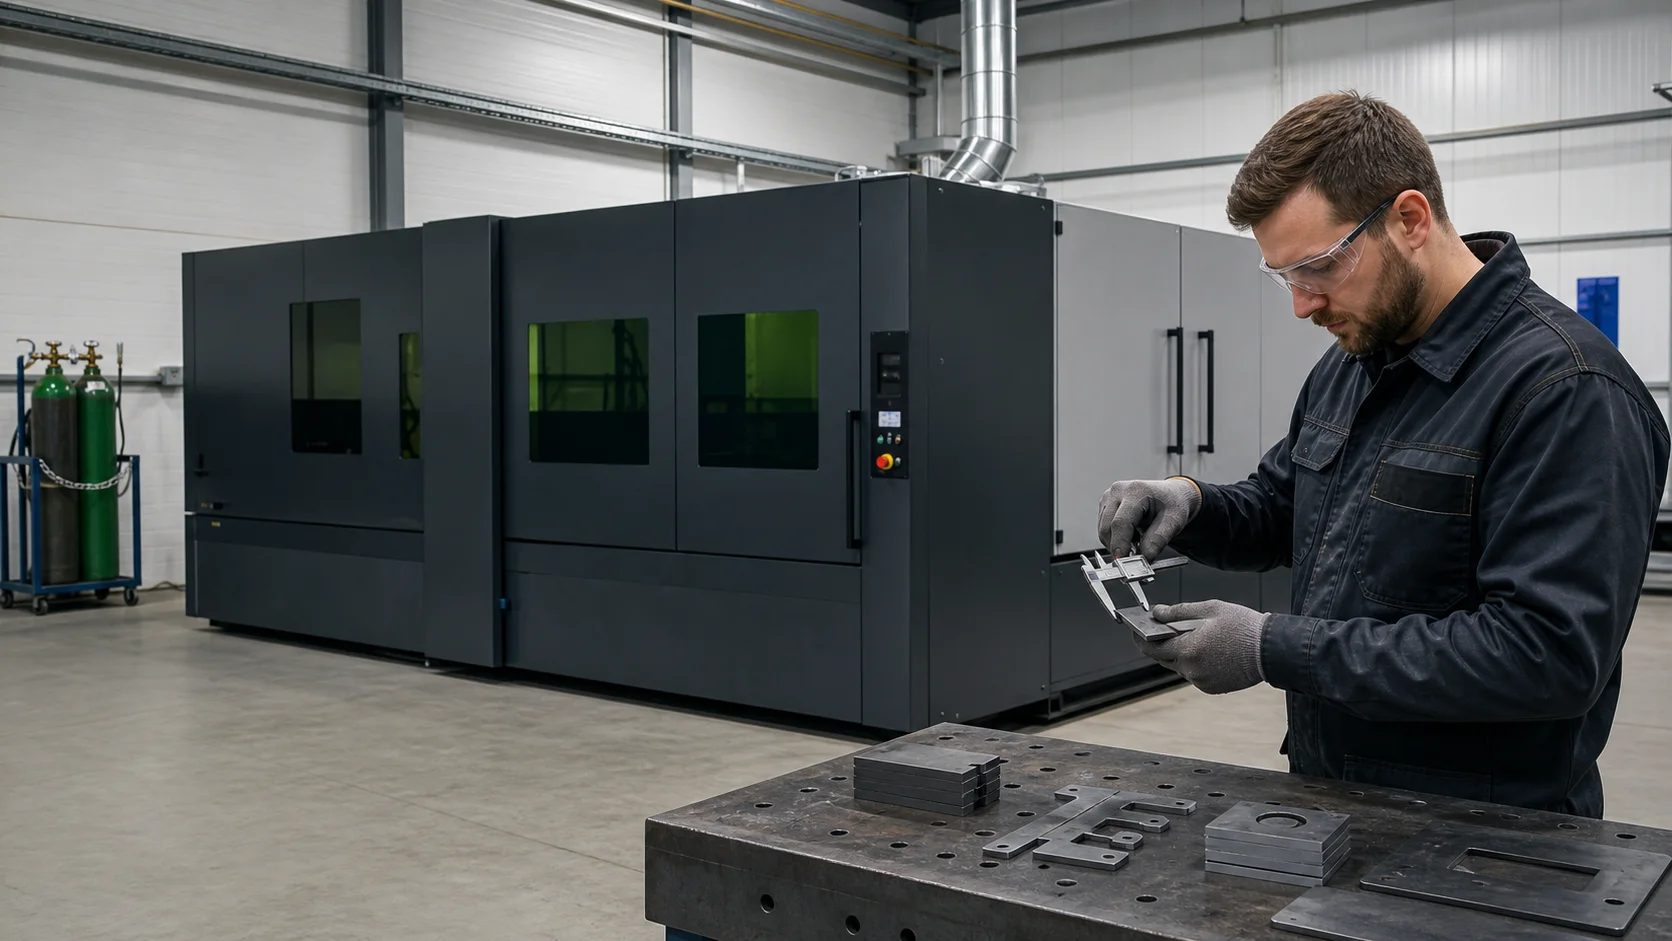
Record material grade, thickness, surface condition, part file, gas, nozzle, focus, speed and power. Photograph both faces of the cut and note whether the fault follows one direction, one area of the sheet or a specific operation. Compare with the last known acceptable sample before changing settings.
Separate likely causes from symptoms
Burr or dross can involve focus, speed or gas delivery. Rough edges can also involve material condition or motion. Incomplete cuts require checking the approved recipe, gas and nozzle condition before assuming a source fault. Unstable piercing calls for a review of the piercing sequence, height and gas. These are investigation paths, not a universal diagnosis or a pressure/power recipe.
Test one change at a time
Use the manufacturer's approved procedure to check nozzle condition and centering, protective-window condition, height response and gas delivery. Compare measured gas pressure under flow with the required supply condition; a static gauge reading alone is insufficient. Within the approved process limits, change one setting, cut the same test geometry and log the result. Restore the last known configuration if the result deteriorates.
Know when to stop and escalate
Stop for safety-interlock faults, damaged optics, abnormal head heating, cooling alarms or suspected source/fiber damage. Do not bypass guards or open optical assemblies outside the authorized maintenance procedure; follow the manufacturer's isolation instructions and use qualified service personnel. Close the investigation only after repeated representative parts meet the agreed edge, piercing and dimensional criteria, with the final settings and cause recorded.
Fiber Laser Cutting Quality Troubleshooting Guide: Burrs, Dross, Rough Edges and Incomplete Cuts
Should an operator increase laser power first when cuts become poor?
No. First make the machine safe, then inspect the documented process conditions and physical causes. More power can worsen a problem caused by focus, gas, nozzle condition, height control or material variation.
How can an operator separate a focus or nozzle problem from a normal burr on a fiber laser cut?
Compare a known-good sample, inspect approved nozzle and focus settings, and test one variable at a time. Burr alone cannot identify the cause without process and material records.
When should gas pressure, flow and purity be checked before changing the cutting program?
Check gas delivery early when quality changes across otherwise identical jobs, especially under flow. Verify pressure, flow and purity before compensating with cutting parameters.
When must contaminated optics, source faults or unsafe cutting-head work be escalated to qualified service personnel?
Escalate damaged or contaminated internal optics, suspected source/fiber faults, abnormal heating, cooling or safety alarms. Stop and follow the manufacturer's isolation and authorized service procedures.
Related technical guides
Official technical references
Platform names describe product families, not guaranteed retrofit compatibility. Final software, controller and license selection follows a machine survey.