Prepared by: Arkmex · Content updated:
General planning guidance; a machine-specific survey and the agreed technical scope take precedence. Official references are listed below.
Engineering takeaways
- The conversion changes wavelength, beam delivery, optics, cooling load and process behavior; it is not a resonator swap.
- A successful retrofit starts with measured machine condition and documented interfaces, not a controller shopping list.
- Retain a tested rollback path until safety, motion, process and production acceptance are complete.
Compatibility checklist
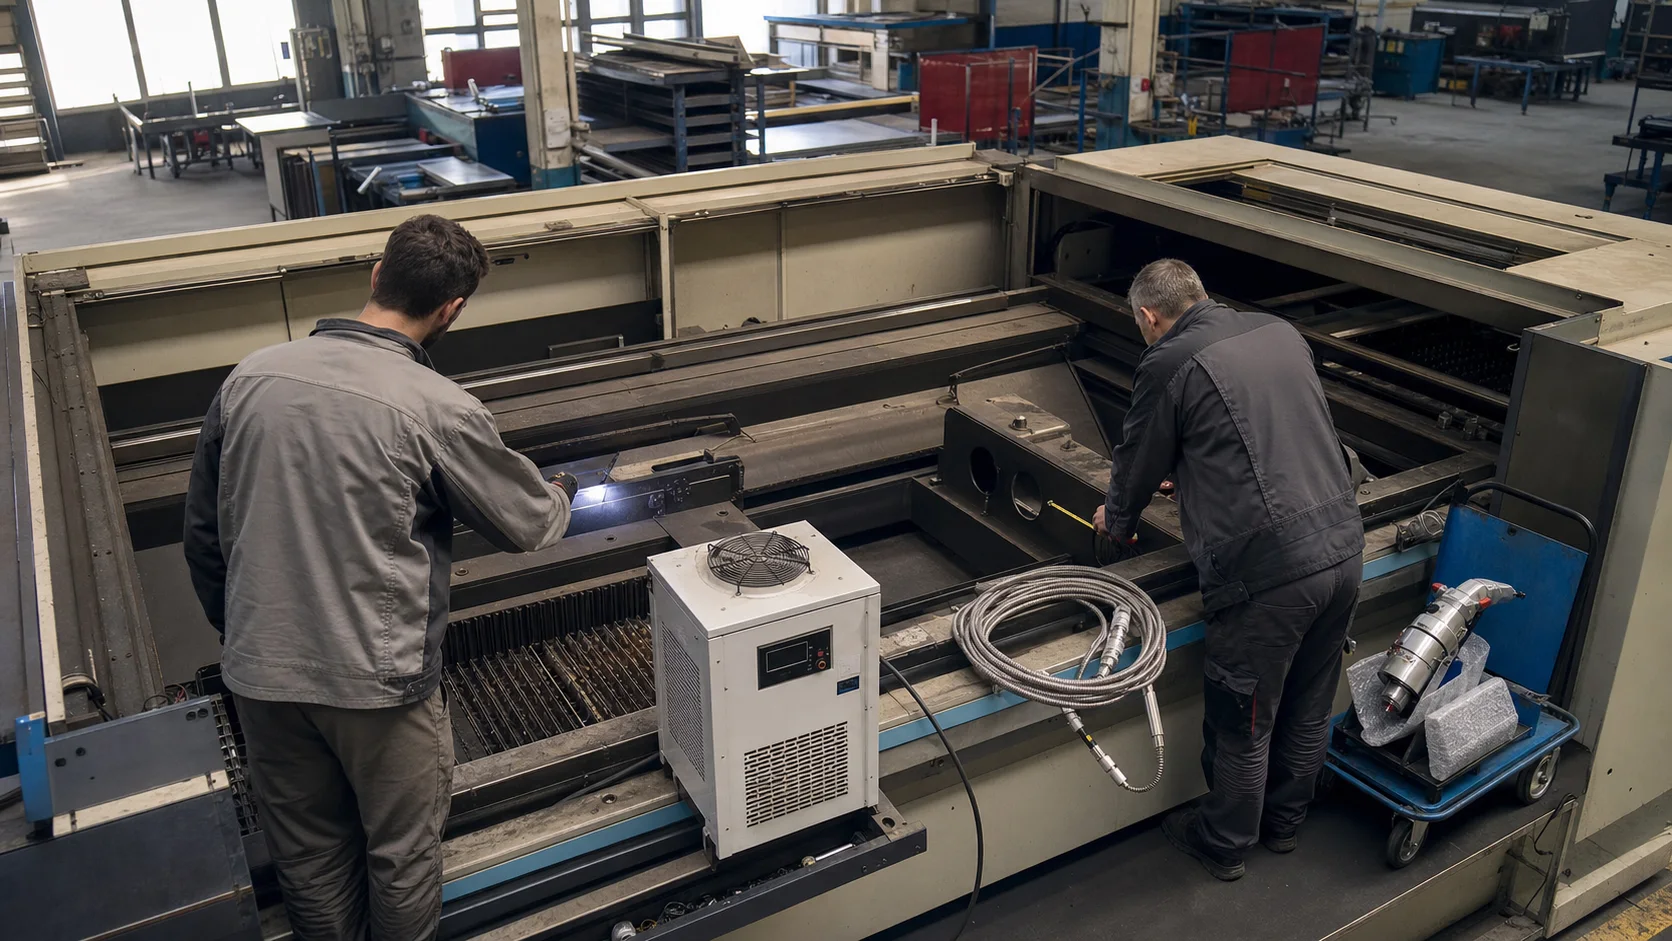
- Evaluate whether a mature TRUMPF CO2 machine can accept a fiber source, new cutting head, cooling, gas, electrical and control architecture without overstating the retained machine's capability.
- Record machine model, serial number, year, working area and automation options.
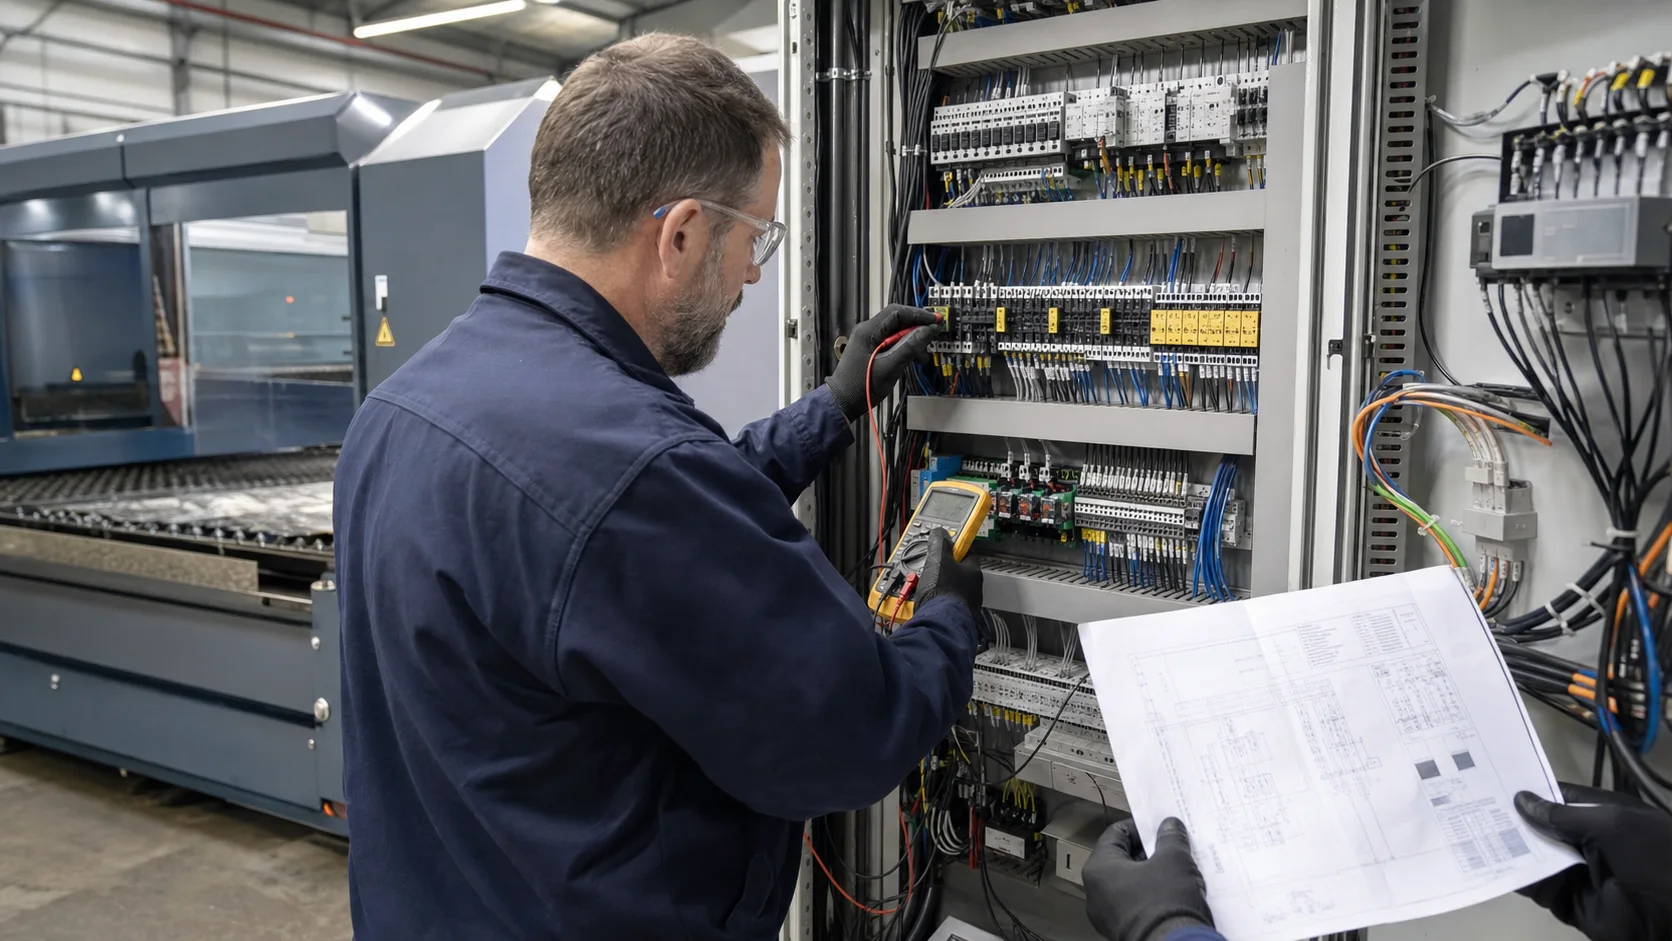
- Identify controller, industrial PC, servo drives, encoders, fieldbus, remote I/O and height-control hardware.
- Collect electrical, pneumatic, gas, cooling, extraction and safety drawings; mark undocumented changes.
- Measure mechanical accuracy, backlash, gantry squareness, slat-bed condition and axis performance before increasing speed or power.
- Define materials, thickness range, assist gases, daily output, quality limits and target laser power.
Hardware and integration scope
- Plan the fiber source, armored fiber, compatible head, chiller, gas train, extraction, electrical capacity and controller together.
- Industrial PC or operator console, controller and licensed software matched as one supported set.
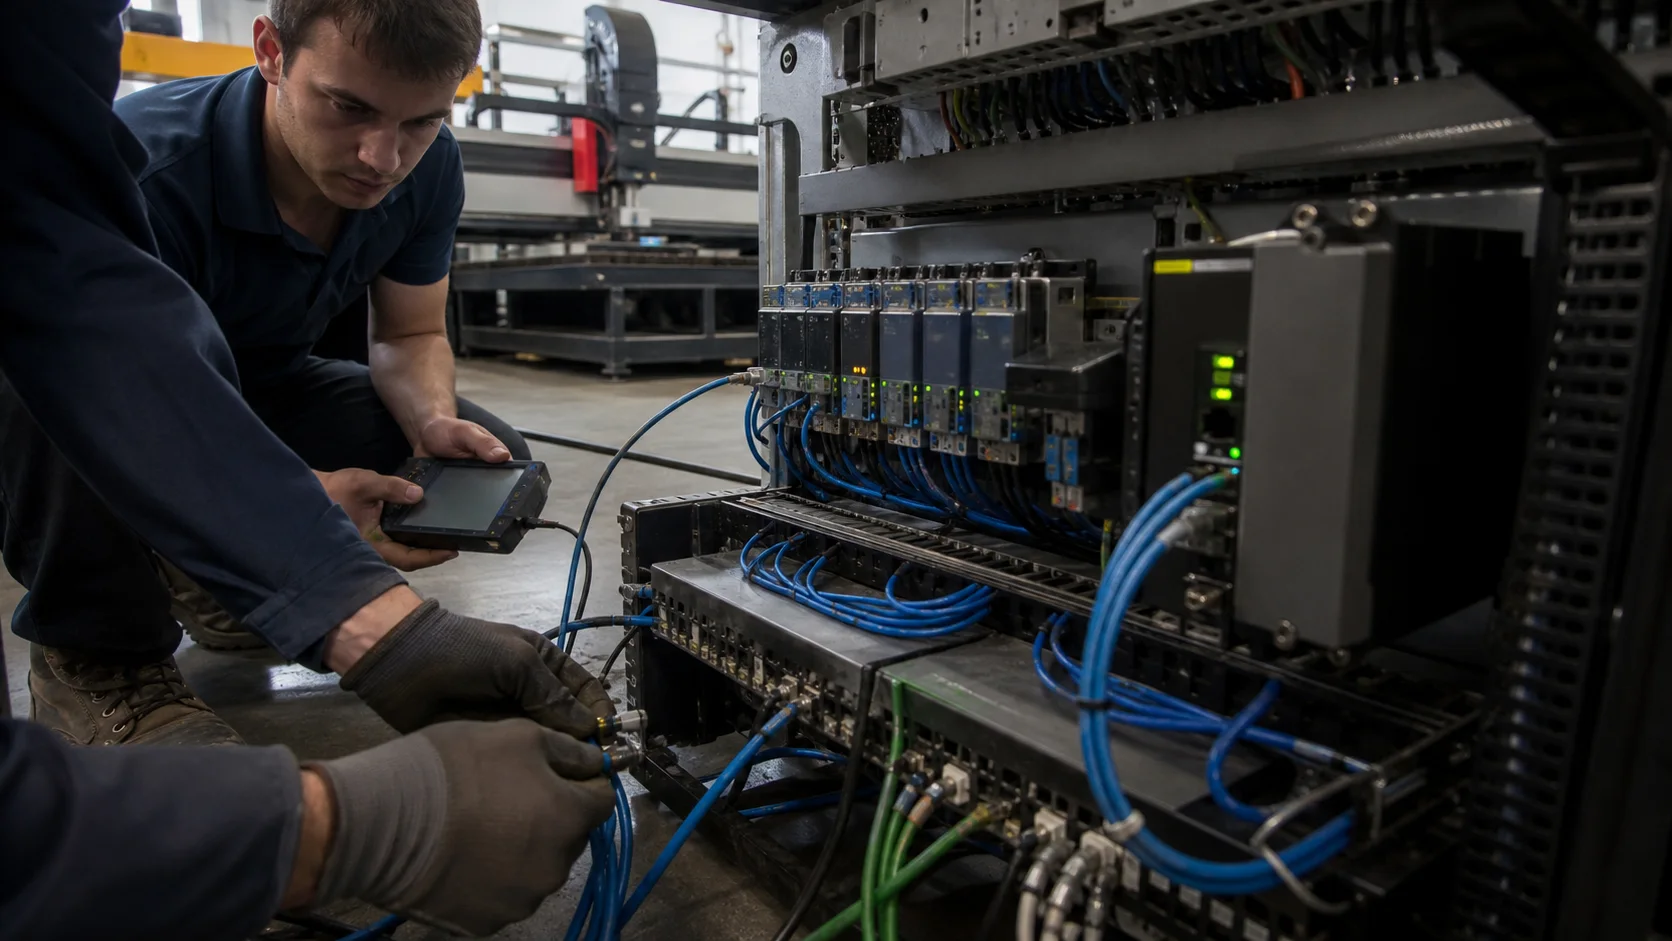
- Servo/encoder interfaces, fieldbus couplers, remote I/O, safety relays and galvanic isolation where required.
- Capacitive height control, cutting-head signals, laser modulation, gas valves, chiller and extraction interlocks.
- Documented terminal numbering, cable shielding, grounding, spare I/O and service access for future maintenance.
Implementation workflow
- 01
Define the decision: Record machine model, serial number, year, working area and automation options.
- 02
Capture the machine baseline: Evaluate whether a mature TRUMPF CO2 machine can accept a fiber source, new cutting head, cooling, gas, electrical and control architecture without overstating the retained machine's capability.
- 03
Freeze the integration architecture: Plan the fiber source, armored fiber, compatible head, chiller, gas train, extraction, electrical capacity and controller together.
- 04
Prepare the outage: Issue the retrofit architecture, I/O matrix, bill of materials, risk register, rollback plan and outage schedule.
- 05
Commission through controlled gates: Reflective-material capability and higher speed may exceed the old enclosure, extraction, slat bed or motion system. Commission axes at low speed, tune following error and height control, validate gas and laser signals, then build process tables progressively.
- 06
Prove production acceptance: Compare energy use, cut quality, repeatability and cycle time against agreed materials—not against a new-machine brochure.
Detailed engineering notes
Decision boundary
Review the enclosure, viewing windows and protective measures for the selected fiber wavelength. Existing CO2-era guarding is not evidence of suitability; include the qualified safety assessment in the conversion scope.
Reusable assets and integration limits
The frame, gantry, rails, drives, motors, extraction, gas train and automation should be assessed independently. A part that powers on is not automatically suitable for higher acceleration, a different control loop or higher laser power.
Interface evidence
Identify controller, industrial PC, servo drives, encoders, fieldbus, remote I/O and height-control hardware. Industrial PC or operator console, controller and licensed software matched as one supported set.
Safety case
Trace emergency stops, enclosure doors, light curtains, laser-enable chain, gas pressure, cooling flow, extraction and motion brakes. Each device needs a defined safe response and a recorded validation test after wiring changes.
Controlled commissioning
Verify power distribution and protective earth first, then I/O, fieldbus, axis direction, limits, homing, low-speed motion, servo tuning, height control, gas, laser enable and finally cutting. Do not combine first motion and first laser emission into one test.
Production proof
Use the customer's normal materials, thicknesses and quality criteria. Record nozzle, focus, gas, power, speed, piercing and inspection results, then compare repeatability across more than one sheet.
Handover and support
Train operators on daily use and maintenance staff on backups, alarms, I/O diagnostics and safe replacement procedures. Store the final drawings and software image in at least two controlled locations.
Risks and limitations
- Reflective-material capability and higher speed may exceed the old enclosure, extraction, slat bed or motion system.
- A new controller cannot correct worn rails, backlash, frame distortion or an unstable cutting bed.
- Bypassed or incompletely mapped interlocks create unacceptable personnel and equipment risk.
- Unverified licenses, firmware, servo compatibility or undocumented OEM logic can extend downtime.
Acceptance criteria
- Compare energy use, cut quality, repeatability and cycle time against agreed materials—not against a new-machine brochure.
- All emergency stops, doors, light curtains, pressure, cooling and extraction interlocks stop hazardous motion or laser emission as designed.
- Axis travel, homing, limit switches, following error, repeatability and contour accuracy meet the agreed baseline.
- Cut coupons cover representative materials and thicknesses, including holes, corners, common-line cuts and piercing.
- Backups, drawings, parameter sets, licenses, spare-parts list, operator training and maintenance handover are complete.
TRUMPF CO2 to Fiber Laser Conversion Guide
Will a CO2-to-fiber conversion perform like a new fiber machine?
Not automatically. Source efficiency may improve, but acceleration, enclosure, automation, extraction and mechanical accuracy remain constrained by the retained platform.
Which CO2 optical-path parts are removed during fiber conversion?
Survey the CO2 resonator, mirrors and beam-delivery assemblies. Identify what must be removed or replaced for the selected fiber architecture; do not reuse CO2 optics by assumption.
Does the existing cutting head mount accept the selected fiber head?
Measure the mounting pattern, working height, travel and clearance. Confirm head mass, optical connection and height-control integration before designing an adapter.
Which chiller, gas and extraction changes are needed for fiber cutting?
Size cooling to the source and head specifications; verify gas pressure and flow at the machine, electrical capacity and extraction for the planned materials and duty cycle.
Can the final hardware be selected from photos alone?
No. Photos help identify the machine, but drawings, controller/drive data, I/O measurements, safety logic and mechanical checks are required before a binding scope.
How is retrofit downtime controlled?
Pre-engineering, cabinet preparation, software staging and acceptance planning are completed before shutdown. The schedule still includes contingency for undocumented wiring or failed legacy parts.
Related technical guides
Official technical references
Platform names describe product families, not guaranteed retrofit compatibility. Final software, controller and license selection follows a machine survey.