Prepared by: Arkmex · Content updated:
General planning guidance; a machine-specific survey and the agreed technical scope take precedence. Official references are listed below.
Engineering takeaways
- Start with the parts you must produce and the output you need—not the highest available power rating.
- Size the machine around everyday production thickness, not an occasional maximum.
- Approve a power choice with representative parts and measured cycle costs.
Build a material and thickness schedule
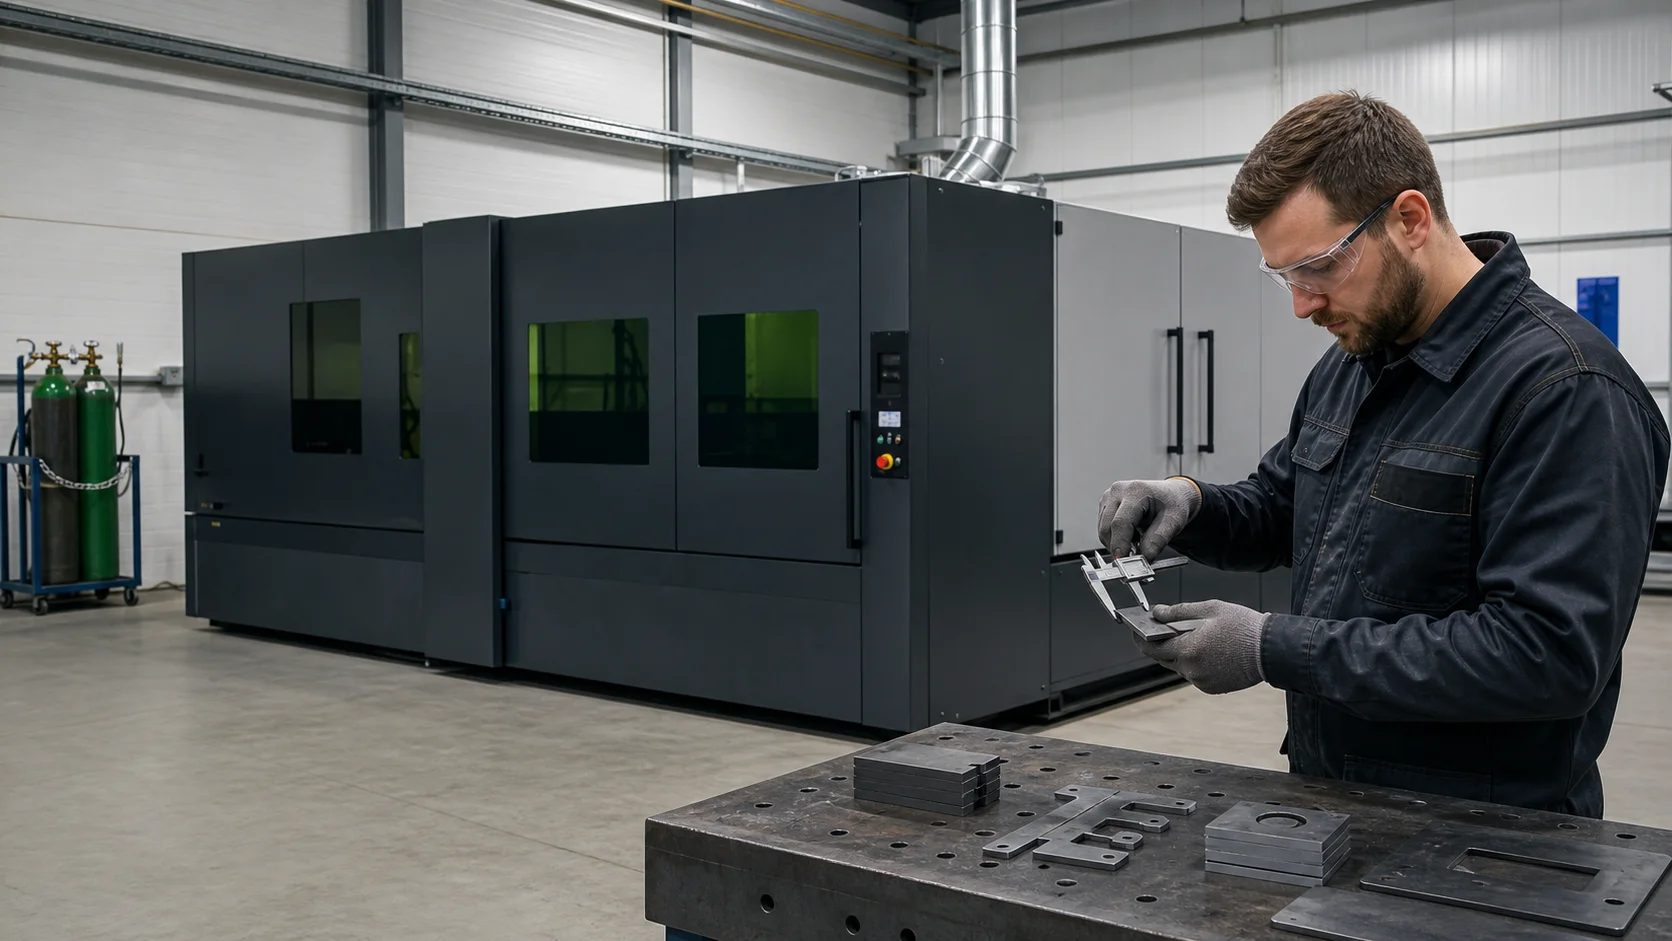
List material grade, normal thickness, maximum thickness, part dimensions and daily quantity. Separate stainless steel, carbon steel and aluminum instead of assigning one thickness capability to all metals. Record edge finish, burr tolerance, small holes and subsequent welding or coating needs. These requirements determine whether a reference cutting range is useful for your production.
Check the complete production system
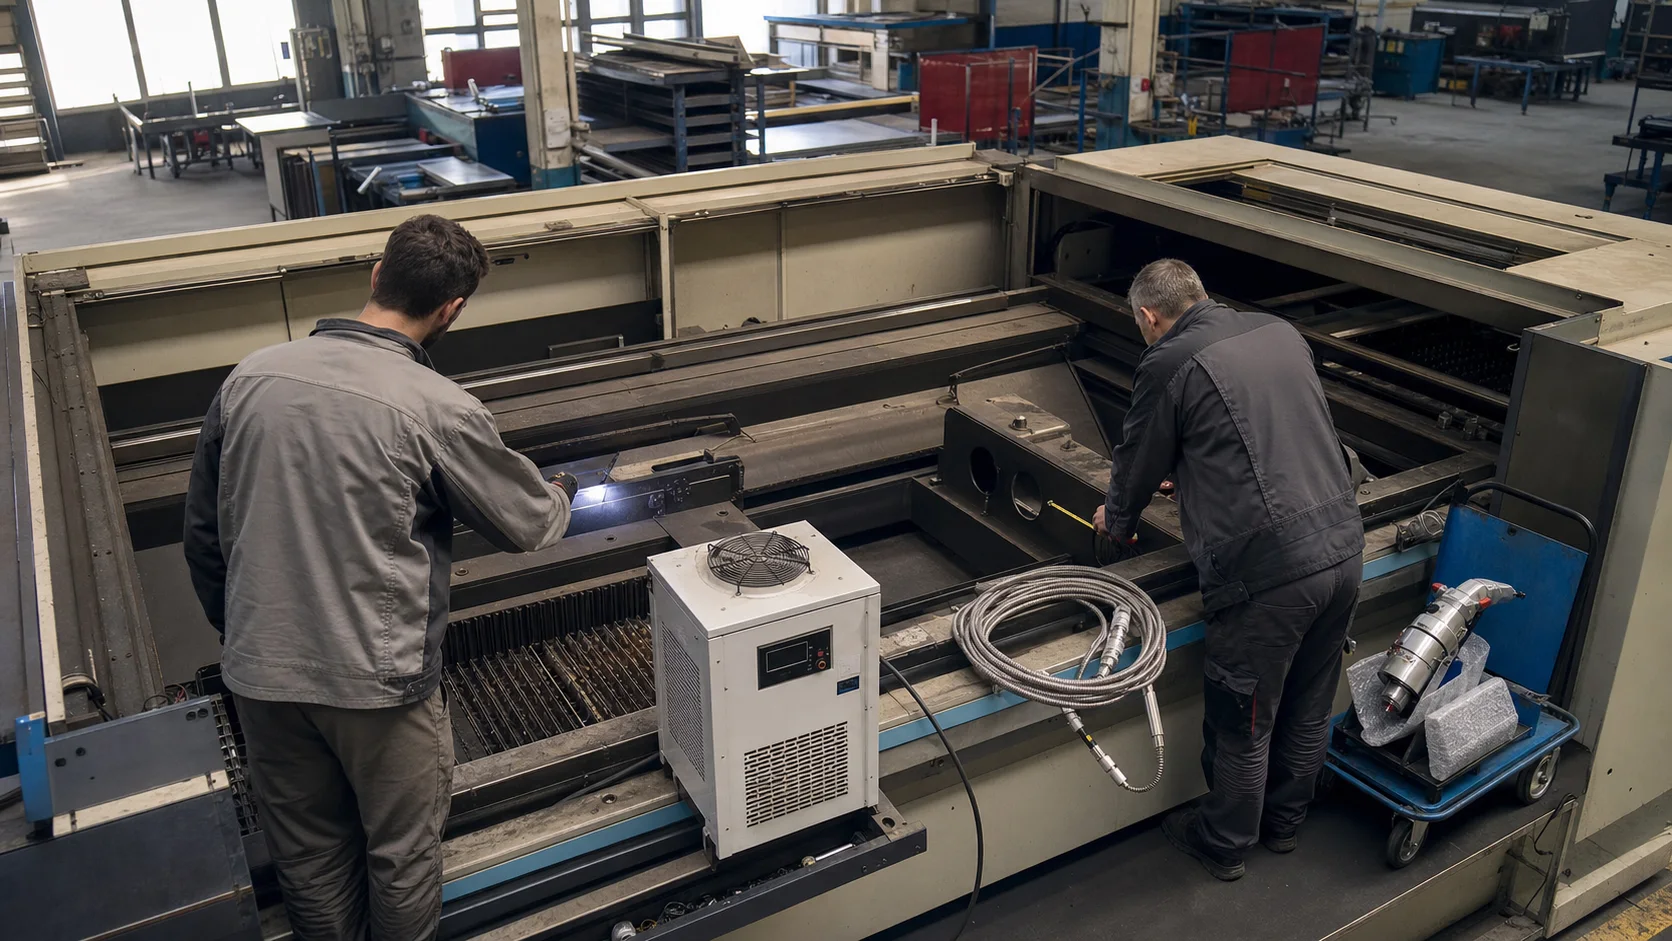
Match the source with the cutting head, cooling, electrical supply, assist-gas capacity and extraction. Confirm loading, unloading and available floor space. For tubes, record diameter, wall thickness, length and profile separately; AX-6000T's Ø10–350 mm specification refers to round tube diameter. More power does not remove handling delays or correct worn mechanics.
Compare sample cutting on equal terms
Use the same material grade, thickness, part file and acceptance criteria for each proposed power level. Record gas type, nozzle, focus, piercing time, cutting time and total cycle time including handling. Compare accepted parts per hour and variable cost per accepted part; do not rank machines solely by straight-line cutting speed.
Set the purchase acceptance criteria
Agree the tested materials, typical thicknesses, edge quality, hole quality, throughput and utility conditions in the quotation. A maximum-thickness demonstration does not establish continuous production capacity. Repeat representative parts and record rejected pieces. Choose the configuration that meets the agreed workload with support and operating costs your team can sustain.
How to Choose Fiber Laser Cutting Machine Power for Metal Thickness and Production Goals
Is the highest laser power always the best choice for a buyer?
No. Higher power can improve the useful production window for some jobs, but the best configuration is the one that meets the agreed part mix, throughput, quality, utilities and budget with a supportable process.
How should a buyer match fiber laser power to a mixed stainless-steel and mild-steel part program?
Compare each material grade and its typical thickness separately, weighted by production volume; test the proposed configuration on the actual mix before choosing power.
Why should maximum thickness be separated from the thickness used in daily production?
Maximum thickness is a boundary demonstration; normal production also needs repeatable quality, acceptable cycle time, consumable life and utility capacity over sustained work.
Which gas, electrical and extraction requirements must be confirmed before choosing a higher-power machine?
Confirm gas pressure, flow and purity at cutting demand, complete electrical load, cooling duty and extraction. Have qualified personnel validate supply and protection requirements.
Related technical guides
Official technical references
Platform names describe product families, not guaranteed retrofit compatibility. Final software, controller and license selection follows a machine survey.